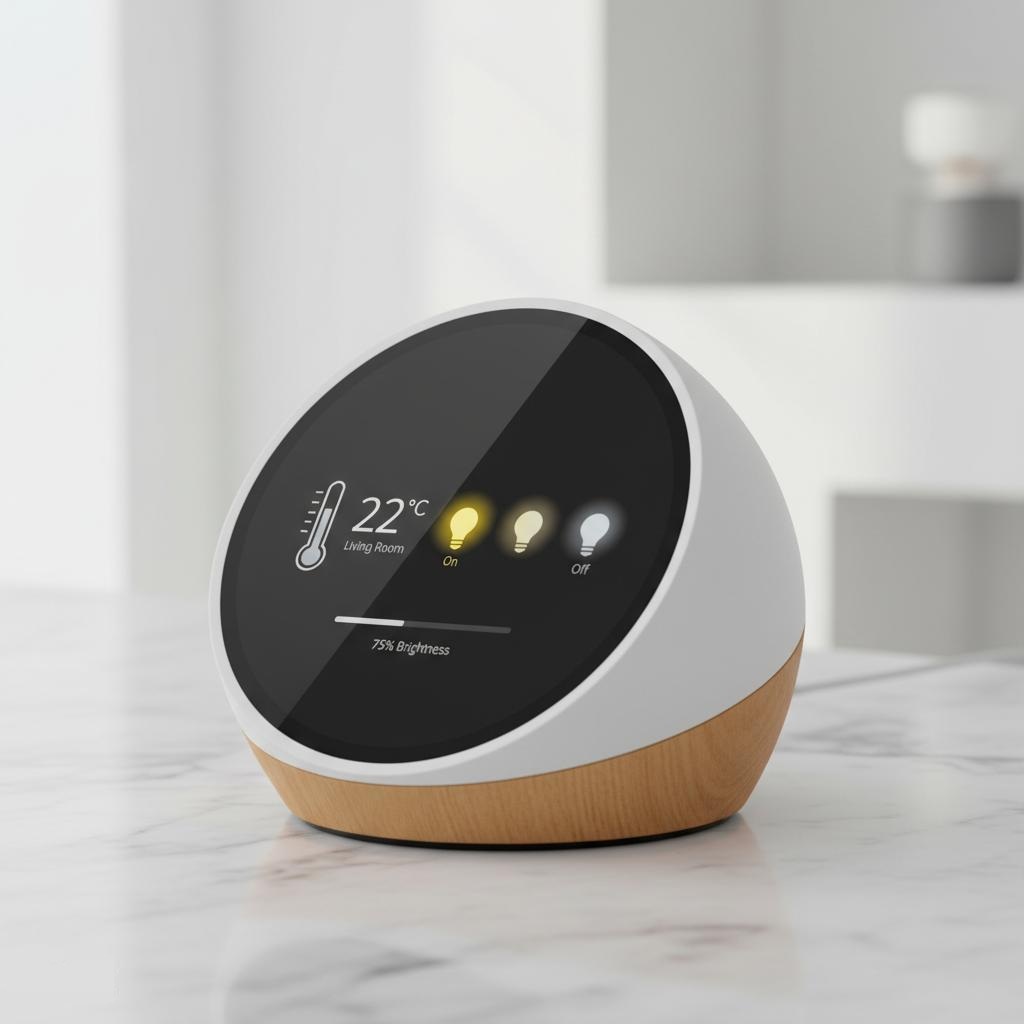
Last October, a founder named Theo walked into our Shenzhen office with a prototype that made everyone in the room lean in. It was a palm-sized "pebble" — a smart kitchen timer and scale hybrid called Crumble. Soft to the touch. Seamless. It had passed a drop test, a 30-minute water dunk, and a full functional sweep. He'd raised $240K on that object and signed a letter of intent for 5,000 units with a US retailer. "We're cutting tooling in three weeks," he said. "We just need a factory."
I remember the silence after our lead engineer turned the part over in his hand.
Theo's prototype wasn't lying on purpose. But it was lying. The "soft-touch" skin was a hand-sprayed rubber coating over an SLA-printed core. The "waterproof" seam was glued, not welded. The inductive charging coil sat exactly where Theo's fingers happened to place it. None of that could survive a steel mold or a production line — and none of it showed up in the test report that convinced his investors.
Here's the thing most founders don't want to hear: a 3D printed prototype is not a small version of your product. It's a small version of your idea. And ideas and products are separated by every lesson your prototype refused to teach you.
At SciPure, our founder came out of the Foxconn-Apple joint lab — 20 years of taking consumer electronics from a CAD file to tens of millions of identical units, 29 granted patents landed along the way, and a 2020 Shenzhen science-and-technology leadership award to show for it. We've run 127 product programs since 2024. In 73% of them, the founder arrived holding a "production-ready" 3D print that was quietly hiding problems a steel mold would have exposed the hard way. This article is the protocol we wish every one of them had read before they signed a tooling purchase order.
The Brutal Truth About What a 3D Print Actually Is
Look, we get it. 3D printing is magic. You design on Monday, hold the part on Wednesday, test it on Friday. No tooling, no minimum order, no six-week wait. For asking questions about your design, nothing beats it.
The trap is treating the answer to "does this shape work?" as the answer to "can this be manufactured?" Those are different questions. 3D printing is a question-asking tool. Injection molding is an answer-scaling tool. The only real mistake is paying for the scaling answer before you've finished asking the questions.
And here's the part that stings: your prototype looks so finished that it feels like a product. It isn't. It's a convincing costume your idea wears to the investor meeting.
The Five Lies Your Prototype Is Telling Your Factory
When we run a pre-tooling review, these are the five deceptions we catch most often. Every one of them can turn a clean tooling quote into a six-figure disaster.
Lie #1: The Material Lie
Your SLA print is printed in a UV-cured resin. Your FDM print is laid down in strands. Your real product will be molded in PC/ABS, or glass-filled PA, or TPE overmold. Those are not the same material, and they do not behave the same way.
Industry data is blunt: FDM parts in engineering-grade filament reach only 60–70% of the tensile strength of the same molded resin. Across additive processes broadly, 3D-printed strength runs 60–90% of molded, and it's anisotropic — weaker along the build axis, because layer lines are tiny internal fault lines. Injection-molded parts are isotropic and solid. For a founder counting on a snap-fit that holds for 10,000 cycles, that 30–40% gap is the difference between a product and a recall.
Lie #2: The Process-Variance Lie
Your SLA print had no draft angle, no parting line, and three undercuts — because the printer doesn't care. A mold cares deeply. Those features are either impossible to eject, or they demand side-actions and lifters that can double tooling cost.
Tolerances tell the same story. A 3D print holds roughly ±0.1–0.5 mm. A well-controlled mold holds ±0.02–0.05 mm — routinely, part after part. If your product mates with a screen, a gasket, or another molded half, the prototype's sloppy tolerance is hiding a fit problem you'll discover at first article inspection.
Lie #3: The Assembly Lie
This is the one that burns founders. Theo's "seamless waterproof pebble" was glued shut by hand. His "soft-touch" surface was sprayed on. The coil was positioned with a jig and a prayer. None of those is a manufacturing process. They're prototype shortcuts — manual steps a production line cannot repeat 5,000 times.
When we see a prototype held together by adhesive, tape, or wire, we don't see a finished product. We see a list of processes that still have to be designed: ultrasonic welding, two-shot overmolding, press-fit alignment, automated coil placement. Each one is a DFM decision your print let you skip.
Lie #4: The Cosmetic-at-Scale Lie
On the bench, your print looks premium. Under a production run, the truth shows up. Sink marks appear where wall thickness jumps. Class-A surfaces that an SLA shell faked with filler and sanding reveal layer lines or witness marks at scale. Textures that looked "soft-touch" in resin show flash and short shots in TPE.
Cosmetic failures are the most expensive kind of invisible problem, because they pass functional testing and fail on the shelf — in front of customers, on Amazon, where a 1-star "looks cheap" review compounds forever.
Lie #5: The Cost-at-Scale Lie
This is the lie that quietly kills margins. Your prototype cost you $40 in machine time. You assume production costs about the same. It doesn't.
3D printing has zero tooling but a high, flat per-part cost — typically $5–$50 per unit that never comes down. Injection molding flips that: $3,000–$50,000+ in tooling once, then $0.05–$5 per part that keeps falling. The crossover point lands around 500–2,000 units for medium-complexity parts. Below that, your print was the right call. Above it, the print is lying about your business model.
And in August 2026, that lie has a tariff on top of it.
The Tariff Time-Tax Nobody Budgets For
Here's the dimension most founders miss when they cost-model off a prototype. As of July 24, 2026, the US Section 301 forced-labor tariff went live at 12.5% on Chinese-origin goods (10% for a small group of economies with stronger enforcement). Stacked on the existing China-specific Section 301 duties, the cumulative burden on consumer electronics shipping from China now sits at roughly 37.5% — and a coalition of 25 states is already in court trying to block it while Customs keeps collecting.
What that means for your prototype's cost lie: a design that's marginally viable at $31/unit becomes a loss-maker the moment +37.5% lands on the landed cost. The "cost at scale" deception isn't just about molding vs printing anymore — it's about whether your product survives a duty stack it was never designed to absorb. If your margin model assumes pre-2026 tariff math, your prototype is lying to your CFO.
A Question Every Founder Should Ask Before Tooling
We use a simple decision tree with every client. Find the line that sounds like you:
- If you need fewer than 500 units and the geometry is weird → 3D printing or bridge tooling is correct. Do not cut steel yet. You're still asking questions.
- If you've funded a campaign and have 1,000+ committed backers → get an independent DFM review before the mold. Your supplier's "it's fine" is not a design review.
- If your prototype passed every test but was printed, not molded → assume 7–14 hidden issues. Budget a two-week redesign sprint. It will be the cheapest two weeks of the project.
- If you're cost-modeling from the prototype's BOM → your true fully-loaded COGS is 2–3x that number. Re-run it with molding, scrap, QC, freight, and the 2026 tariff stack before you price the product.
The $1,800 Review That Rewrote Theo's Tooling Quote
Theo's pre-tooling review took 20 minutes and cost him $1,800. It found seven issues. Two were mold-killers:
- The overmold needed a parting line and draft his SLA core didn't have — would have required a second side-action, adding ~$9K and 3 weeks.
- The sealed seam, glued on the prototype, needed ultrasonic welding on a surface with zero energy director — a redesign, not a tweak.
The rest: wall thickness swinging from 0.9 to 4.1 mm (sink marks and warpage), a magnet pocket with no steel insert (deformed at 10k cycles), a logo sitting exactly on the parting line (flash across the brand), and a "soft-touch" texture that TPE simply cannot mold as-printed.
Catch those before steel and the fixes were nearly free — a few CAD edits. Catch them after the mold was cut and the same seven issues ran $41,000 to $73,000 in rework, insert changes, and a second tool. That's a 23:1 return on a review most founders skip because "the factory already said it's fine."
How to Fix It: The Prototype-to-Production Honesty Protocol
You don't need to stop 3D printing. You need to stop trusting it. Three moves:
1. Run the Honesty Audit. Before any tooling quote, score your prototype on five flags: Material (is it the real resin?), Process (does it have draft/parting line/uniform walls?), Assembly (any glue/tape/wire/manual placement?), Cosmetic (any filler/sanding/post-process a line can't repeat?), Cost (did you model molding + tariff, or just the print?). Red on any flag = redesign before steel.
2. Choose bridge tooling deliberately. For the 500–5,000 unit valley between prototype and mass production, an aluminum MUD (Master Unit Die) mold runs $3,500–$6,800 and delivers in weeks — versus $15K+ and 6+ weeks for steel. It buys you real molded parts to validate before you commit to the production tool. This is where a print should hand off, not where it should end.
3. Use AI as a screening layer, not a decision-maker. Modern DFM copilots catch 80% of issues instantly and ~95% after a two-week learning pass. AI vision inspection now hits 97–99.4% defect detection versus 70–85% for a human inspector who degrades 15–25% after two hours. These tools widen your margin for error — they do not replace the engineer who has to decide what the part is for. Keep a human in the loop, always.
What Apple's Supply Chain Teaches Us About the Prototype Gap
You might think the answer is to move production out of China and skip the gap entirely. The 2026 Apple supply chain says otherwise. Even after aggressive "China+1" moves, 70–80% of iPhone component value is still made in China. India assembles roughly 25% of iPhones (up from single digits in 2022), and Vietnam handles modules — AirPods, Watch, some Mac — not the precision tier. When a high-end model needed capacity in July 2026, the work came back to China.
The reason isn't cheap labor. It's ecosystem depth — the hour-level supplier response that only exists where the whole chain lives in one cluster. The prototype-to-production gap isn't a geography problem. It's an engineering-depth problem. A founder who treats a print as a product will hit that wall in any country. A founder who respects the gap will clear it anywhere.
That's the lesson our founder's two decades inside the Foxconn-Apple joint lab drilled into us: the hardware game is won or lost in the distance between "this one works" and "all of them work, the same way, without us in the room."
A prototype proves your idea can be built once. Manufacturing proves it can be built ten thousand times, the same way, without you there to hold it. The most expensive dollar in hardware is the one you saved by believing your prototype was already the product.
If you have a product concept and want to know if it's manufacturable, send a written brief at www.scipure.net/inquiry.html. We'll review your design and tell you exactly where the risks are.